
Well Check Valve Manufacturer | High-Quality Valve Production Facility
By:Admin
Company News & Blog
High-Quality Full Bore Ball Valve for Sale - Find the Best Deals Now!
The importance of reliable and high-quality industrial valves cannot be overstated in various industries such as oil and gas, petrochemical, water and wastewater, and power generation. These industries require durable and efficient valves to control and regulate the flow of various fluids within their processes. To meet this need, the leading valve manufacturer, {Company Name}, is pleased to introduce their innovative Full Bore Ball Valve, designed to provide unrivaled performance and reliability in the most demanding industrial applications.The Full Bore Ball Valve offered by {Company Name} is engineered to allow for full flow of fluids, minimizing pressure drop and ensuring efficient performance. This valve is designed with a robust and durable construction, using high-quality materials that can withstand the harshest operating conditions. The valve features a smooth bore, which enables the unobstructed flow of fluids, making it ideal for applications where low pressure drop and minimal turbulence are essential.One of the key advantages of the {Company Name} Full Bore Ball Valve is its versatility and adaptability to various industrial processes. It is suitable for a wide range of media, including corrosive and abrasive fluids, high-temperature and high-pressure applications, and viscous or solid-laden fluids. This makes it a reliable and cost-effective solution for numerous industries that require precision flow control.In addition to its exceptional performance, the Full Bore Ball Valve is engineered to provide easy installation and maintenance. The valve is designed for simple operation and can be easily integrated into existing systems. Its low maintenance requirements make it a practical choice for industries looking to minimize downtime and operational costs.{Company Name} takes pride in its commitment to delivering exceptional quality and reliability with all its products, including the Full Bore Ball Valve. The company has a proven track record of providing innovative and dependable valve solutions to various industries around the world. With a focus on continuous research and development, {Company Name} ensures that its products adhere to the highest industry standards and incorporate the latest technological advancements.Furthermore, {Company Name} offers unparalleled customer support and technical assistance, ensuring that clients receive comprehensive support in selecting, installing, and maintaining their valves. The company’s team of experienced professionals is dedicated to providing tailored solutions that meet the specific needs of each client, offering expert advice and guidance throughout the entire process.The introduction of the Full Bore Ball Valve further solidifies {Company Name}’s position as a leading global provider of industrial valve solutions. By combining innovation, quality, and exceptional customer service, {Company Name} continues to set the standard for reliable and efficient valve technology in the industry.As industries strive to optimize their processes and maximize efficiency, the demand for high-performance valves has never been greater. With the Full Bore Ball Valve, {Company Name} delivers a solution that exceeds expectations and provides a reliable, long-term investment for industrial operations worldwide.In conclusion, the Full Bore Ball Valve introduced by {Company Name} represents a significant advancement in valve technology, offering unparalleled performance, durability, and versatility. With a strong emphasis on quality, innovation, and customer satisfaction, {Company Name} continues to be at the forefront of providing reliable valve solutions to industries worldwide. As the industry evolves, {Company Name} remains committed to meeting the changing needs of its clients and delivering cutting-edge valve technology that sets new standards for excellence.
Air Flow Control Valve: Everything You Need to Know
Air Flow Control Valve Improves Efficiency and Performance in Industrial ApplicationsIndustrial machinery and equipment require precise control of air flow to ensure optimal performance and efficiency. One company that is at the forefront of providing innovative air flow control solutions is {Company Name}. With over 20 years of experience in the industry, {Company Name} has established itself as a leading provider of high-quality valves and controls for a wide range of industrial applications.The latest product offering from {Company Name} is the Air Flow Control Valve, which is designed to deliver exceptional precision and reliability in controlling air flow in industrial systems. This advanced valve is engineered to provide smooth and accurate control over the flow of air, allowing for optimal performance and efficiency in a variety of industrial processes.The Air Flow Control Valve features a durable and corrosion-resistant construction, making it suitable for use in demanding industrial environments. Its compact design and modular construction make it easy to install and integrate into existing systems, minimizing downtime and production disruptions. With a wide range of available sizes and configurations, this valve can be tailored to meet the specific requirements of different applications, ensuring a perfect fit for any industrial system.One of the key advantages of the Air Flow Control Valve is its precise and responsive control capabilities. The valve is equipped with advanced actuation technology that enables fast and accurate adjustments to the air flow, allowing for precise regulation of pressure and flow rates. This level of control is essential for maintaining consistent performance and achieving optimal efficiency in industrial processes.In addition to its superior control capabilities, the Air Flow Control Valve is also designed for long-lasting durability and reliability. With high-quality materials and components, this valve is built to withstand the rigors of industrial operation, providing years of dependable performance with minimal maintenance requirements. This reliability is essential for ensuring uninterrupted production and minimizing costly downtimes in industrial facilities.{Company Name} takes pride in its commitment to delivering exceptional quality and performance in all of its products, and the Air Flow Control Valve is no exception. Each valve is subjected to rigorous testing and quality control measures to ensure it meets the highest standards for performance and reliability. This dedication to quality has earned {Company Name} a reputation for excellence among industrial customers.The Air Flow Control Valve is just one example of {Company Name}'s dedication to innovation and customer satisfaction. The company continuously invests in research and development to bring cutting-edge solutions to the market, and it collaborates closely with customers to understand their unique needs and challenges. This customer-centric approach allows {Company Name} to develop tailored solutions that address specific requirements and deliver tangible benefits to industrial operations.With a global presence and a strong network of technical experts and support personnel, {Company Name} is well-positioned to serve the needs of industrial customers around the world. Whether it's helping customers select the right valve for their application, providing technical support, or offering maintenance services, {Company Name} is committed to being a reliable partner throughout the life cycle of its products.In conclusion, the Air Flow Control Valve from {Company Name} represents a significant advancement in air flow control technology for industrial applications. Its precision, reliability, and durability make it an ideal choice for a wide range of industrial processes, helping customers achieve optimal performance and efficiency. With a focus on quality, innovation, and customer satisfaction, {Company Name} continues to set the standard for excellence in the industrial valve and controls industry.
Latest Innovations in NRV Valve Technology and Applications
Nrv Valve, A Leading Player in Industrial Valve SolutionsNrv Valve, a prominent player in the industrial valve solutions sector, has been making waves with its innovative and high-quality products. The company has established itself as a go-to provider for a wide range of industries, including oil and gas, petrochemical, power generation, and water treatment. With a strong commitment to excellence and customer satisfaction, Nrv Valve has built a solid reputation for delivering reliable and efficient valve solutions.Founded in [year], Nrv Valve has quickly risen to prominence in the industry, thanks to its focus on innovation and continuous improvement. The company's state-of-the-art manufacturing facilities and advanced R&D capabilities enable it to develop cutting-edge valve solutions that meet the evolving needs of its customers. Nrv Valve's team of experienced engineers and technicians work tirelessly to design, test, and optimize its products, ensuring they meet the highest standards of quality and performance.Nrv Valve offers a comprehensive range of industrial valve solutions, including gate valves, globe valves, check valves, and ball valves, among others. These products are designed to withstand the harshest operating conditions and deliver superior performance and reliability. Nrv Valve's valves are widely used in critical applications, such as controlling the flow of fluids in pipelines, regulating pressure in process systems, and isolating equipment during maintenance and shutdowns.One of the key differentiators of Nrv Valve is its unwavering commitment to quality and safety. The company adheres to strict quality control measures throughout the entire manufacturing process, from raw material procurement to final product testing. Nrv Valve's valves are built to comply with international standards and certifications, ensuring they meet the most stringent industry requirements. Moreover, the company prioritizes safety in its product designs, incorporating features that minimize the risk of leakage, corrosion, and other potential hazards.Furthermore, Nrv Valve places a strong emphasis on customer satisfaction and partnership. The company works closely with its clients to understand their unique requirements and provide tailored valve solutions that address their specific needs. Nrv Valve's dedicated sales and support teams are committed to delivering exceptional service and support to its customers, ensuring a seamless experience from product selection to installation and maintenance.Nrv Valve also prides itself on its global presence and reach. The company's extensive distribution network and strategic partnerships enable it to serve customers in diverse markets around the world. With a strong focus on international expansion and market penetration, Nrv Valve is well-positioned to capitalize on emerging opportunities and expand its footprint in key regions.In conclusion, Nrv Valve has established itself as a leading player in the industrial valve solutions sector, thanks to its relentless commitment to excellence, innovation, and customer satisfaction. The company's high-quality products, focus on safety and quality, and unwavering dedication to its customers make it a preferred choice for businesses across various industries. With its robust capabilities and global reach, Nrv Valve is poised for further growth and success in the years ahead.
Ultimate Guide to Gate Valves: Everything You Need to Know
Innovation and Excellence in Gate Valve TechnologyThe global industrial landscape is constantly evolving, with companies continuously striving to improve their products and services to meet the demands of the market. One such company that has made significant strides in this relentless pursuit of excellence is {Company Name}, a leading manufacturer of industrial valves and fittings.With a rich history dating back to several decades, {Company Name} has established itself as a trusted name in the industry, known for its commitment to quality, reliability, and innovation. The company's dedication to continuous improvement and customer satisfaction has earned it a strong reputation as a preferred supplier of industrial solutions.One of {Company Name}'s flagship products is its range of gate valves, which play a critical role in regulating the flow of fluid within various industrial applications. Gate valves are commonly used in industries such as oil and gas, water and wastewater, power generation, and chemical processing, where the control of fluid flow is essential for the proper functioning of equipment and processes.{Company Name} understands the importance of providing efficient and reliable gate valves to its customers, and has therefore invested heavily in research and development to enhance the performance and durability of its products. The company's team of engineers and technical experts continually explore new technologies and materials to improve the design and functionality of their gate valves, ensuring they meet the evolving needs of the market.Recently, {Company Name} introduced a new line of advanced gate valves that boast several innovative features aimed at improving performance, longevity, and ease of maintenance. These new valves are equipped with state-of-the-art materials and coatings that enhance corrosion resistance and extend the life of the product, even in the harshest operating conditions.Moreover, the new gate valves incorporate advanced sealing technologies that minimize the risk of leakage and ensure tight shut-off, providing operators with peace of mind and confidence in their equipment's reliability. Additionally, the valves are designed with precision-engineered components to deliver smooth operation and reduce wear and tear, resulting in lower maintenance costs and extended service intervals.In line with {Company Name}'s commitment to customer satisfaction, the new gate valves are available in a variety of sizes, pressure ratings, and end connections to accommodate a wide range of industrial applications. Whether it's for high-pressure steam systems, abrasive slurries, or corrosive chemicals, customers can rely on {Company Name} to provide a reliable and cost-effective solution to meet their specific needs.As part of its dedication to quality and performance, {Company Name} ensures that all its products, including the new gate valves, undergo rigorous testing and quality control measures to meet and exceed industry standards. This commitment to excellence has earned the company various certifications and approvals, further solidifying its position as a trusted and reputable supplier of industrial valves.In addition to its cutting-edge products, {Company Name} prides itself on its customer-centric approach, offering comprehensive technical support, prompt delivery, and responsive after-sales service. The company's team of experienced professionals is readily available to provide expert guidance, assistance, and solutions to its customers, ensuring a seamless experience from inquiry to installation.With its unwavering commitment to innovation, excellence, and customer satisfaction, {Company Name} continues to set the benchmark for gate valve technology in the global industrial market. As the company looks to the future, it remains dedicated to pushing the boundaries of possibility and delivering superior industrial solutions that empower its customers to thrive and succeed in a dynamic and challenging environment.
Reliable Dual Plate Check Valve Services for Your Needs
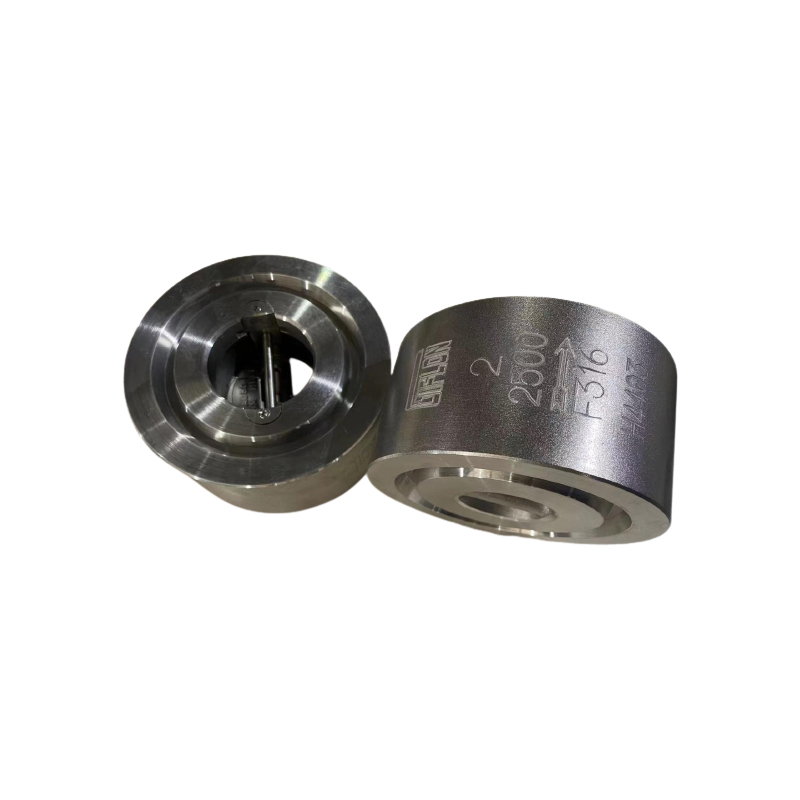
Leading dual plate check valve service provider, {company}, has announced their latest offering, which promises to revolutionize the way industries manage fluid flow control. With a focus on quality and innovation, {company} has established themselves as industry leaders in the valve service sector.With the increasing demand for high-quality valve products in various industries such as oil and gas, water treatment, chemical, and power generation, {company} has been dedicated to providing top-notch dual plate check valve service. Their commitment to quality and customer satisfaction has earned them a stellar reputation in the industry.The dual plate check valve service offered by {company} is designed to offer efficient and reliable fluid flow control solutions for a wide range of applications. The valves are built to withstand high pressure and extreme temperatures, making them ideal for use in demanding environments. In addition, {Company}'s team of experts is trained to provide comprehensive support and maintenance services for their dual plate check valves, ensuring that they continue to perform at their best over time.One of the key advantages of {Company}'s dual plate check valve service is their commitment to innovation and continuous improvement. Their team of engineers and technicians are constantly researching and developing new technologies to enhance the performance and reliability of their valves. This dedication to innovation has allowed {Company} to stay ahead of the competition and deliver cutting-edge solutions to their clients.Furthermore, {Company}'s dual plate check valve service is known for its exceptional quality and reliability. Each valve undergoes rigorous quality control measures to ensure that it meets the highest industry standards. This commitment to quality has earned {Company} certifications and accolades from various regulatory bodies and industry associations.In addition to their top-notch dual plate check valve service, {Company} is also known for their exceptional customer support and after-sales service. Their team of experienced technicians is available to provide expert advice and support to their clients, ensuring that they get the most out of their valve investments. Whether it's installation, maintenance, or troubleshooting, {Company} is dedicated to providing prompt and reliable support to their clients.{Company} takes pride in their commitment to sustainability and environmental responsibility. Their dual plate check valves are designed to minimize leakage and reduce energy consumption, making them an eco-friendly choice for businesses looking to minimize their environmental impact. In addition, {Company} also offers valve refurbishment and upgrade services, allowing their clients to extend the lifespan of their valves and reduce waste.As a leading dual plate check valve service provider, {Company} has established a strong foothold in the global market. Their valves are trusted by some of the biggest names in the industry, and their commitment to excellence has earned them the trust and loyalty of their clients.In conclusion, {Company}'s latest offering of dual plate check valve service is set to raise the bar for fluid flow control solutions. With their focus on quality, innovation, and customer satisfaction, {Company} is poised to remain at the forefront of the industry for years to come. Their commitment to sustainability and environmental responsibility further cements their position as a leader in the valve service sector. Whether it's for oil and gas, water treatment, chemical, or power generation, {Company} is the go-to choice for reliable and efficient dual plate check valve service.
High-Quality Vacuum Check Valve Exporter - Get Your Valves Today!
Vacuum Check Valve Exporter is a leading company in the field of manufacturing and exporting high-quality check valves for various industrial applications. With a strong focus on innovation, quality, and customer satisfaction, the company has established a reputation for excellence in the industry.The company's check valves are used in a wide range of applications, including automotive, medical, aerospace, and environmental industries. They are designed to offer reliable and efficient performance, ensuring the smooth operation of systems and equipment.One of the key factors that set Vacuum Check Valve Exporter apart from its competitors is its commitment to using only the highest quality materials and components in its manufacturing process. This ensures that the check valves not only meet but exceed industry standards, providing customers with a product they can trust.In addition to its dedication to quality, the company also prides itself on its ability to customize check valves to meet the specific needs of its customers. Whether it's a unique size, shape, or performance requirement, Vacuum Check Valve Exporter has the expertise and capability to deliver a tailored solution.Furthermore, the company's strong focus on research and development has resulted in the creation of innovative check valve designs that offer improved performance and efficiency. By staying at the forefront of technological advancements, Vacuum Check Valve Exporter continues to provide its customers with cutting-edge solutions.With a global customer base, Vacuum Check Valve Exporter has a strong presence in the international market. The company's commitment to delivering exceptional products and services has earned it the trust and loyalty of customers around the world.In line with its global reach, Vacuum Check Valve Exporter recognizes the importance of sustainability and environmental responsibility. The company adheres to strict environmental standards in its manufacturing processes and is constantly seeking ways to reduce its carbon footprint.The success of Vacuum Check Valve Exporter can be attributed to its dedicated team of professionals who are committed to upholding the company's values of quality, innovation, and customer satisfaction. The company's employees are highly skilled and experienced, ensuring that every check valve that leaves the facility is of the highest standard.Looking to the future, Vacuum Check Valve Exporter is focused on continued growth and expansion. With an eye towards emerging markets and new technological developments, the company is well-positioned to remain a leader in the industry.The company's dedication to quality, innovation, and customer satisfaction has solidified its reputation as a trusted exporter of vacuum check valves. With a strong emphasis on excellence in all aspects of its business, Vacuum Check Valve Exporter is poised to continue its success as a leading provider of check valves for industrial applications.
High-Quality Gate Valve for Reliable Industrial Applications
Certainly! Please provide the company introduction or any additional details you'd like to include in the news article about the high-quality gate valve.
High-Quality Ball Float Valve for Industrial Applications
ODM Ball Float Valve: A Reliable Solution for Water ControlIn the world of industrial applications, the importance of reliable and efficient water control systems cannot be overstated. Whether it's for maintaining the level of water in a tank, controlling the flow of water in a pipeline, or regulating the water supply in a specific area, having the right tools for the job is essential. This is where the ODM Ball Float Valve comes in.With a focus on precision engineering and innovative design, the ODM Ball Float Valve is a top-of-the-line solution for water control. Its ability to accurately regulate water flow, withstand high pressures, and provide long-term durability makes it the go-to choice for a wide range of industries, including agriculture, oil and gas, water treatment, and manufacturing.The key to the ODM Ball Float Valve's success lies in its design. The valve features a hollow, spherical ball that floats on the surface of the water, connected to a lever arm that opens and closes the valve as the water level changes. This simple yet effective design allows for precise control of water flow, making it ideal for applications where consistent water levels are crucial.In addition to its innovative design, the ODM Ball Float Valve is built to last. Constructed from high-quality materials such as stainless steel and brass, the valve is resistant to corrosion, wear, and tear, ensuring reliable performance even in the harshest conditions. This durability makes it a cost-effective choice for companies looking for a long-term water control solution.Another key feature of the ODM Ball Float Valve is its adaptability. Available in a range of sizes and configurations, the valve can be customized to meet the specific needs of a particular application. Whether it's a small-scale irrigation system or a large industrial water treatment plant, the ODM Ball Float Valve can be tailored to fit the job at hand.The ODM Ball Float Valve is the flagship product of [Company Name], a leading manufacturer of industrial valves and controls. With a strong emphasis on quality, performance, and customer satisfaction, [Company Name] has established itself as a trusted name in the industry.Founded over 20 years ago, [Company Name] has grown from a small local operation to a global provider of cutting-edge valve solutions. With state-of-the-art manufacturing facilities, a team of highly skilled engineers and technicians, and a commitment to continuous improvement, the company is dedicated to delivering products that meet the highest standards of quality and reliability.In addition to the ODM Ball Float Valve, [Company Name] offers a wide range of industrial valves and controls, including gate valves, butterfly valves, check valves, and pressure regulators. Each product is designed and manufactured with the same level of care and attention to detail as the ODM Ball Float Valve, ensuring that customers have access to a comprehensive selection of top-quality solutions for their water control needs.As a company, [Company Name] prioritizes customer satisfaction above all else. From the initial consultation to after-sales support, the company is committed to providing exceptional service at every step of the process. This dedication to customer care has earned [Company Name] a loyal and satisfied customer base, with clients ranging from small businesses to multinational corporations.In conclusion, the ODM Ball Float Valve is a reliable, efficient, and durable solution for water control, backed by the expertise and reputation of [Company Name]. With its innovative design, high-quality construction, and adaptable nature, the valve is well-suited to a wide range of industrial applications. For companies looking for a trusted partner in their water control needs, [Company Name] is the name to remember.
Rubber Lined Gate Valve: Everything You Need to Know
OEM Rubber Lined Gate Valve: A High-Quality Solution for Industrial ApplicationsIn the world of industrial equipment, the need for reliable and durable components is paramount. One such pivotal component is the Rubber Lined Gate Valve, a crucial element in controlling the flow of various substances in industrial settings. These valves play an essential role in ensuring the safe and efficient operation of pipelines and other systems in industries such as oil and gas, water and wastewater, mining, and many others.{Company name} is a leading manufacturer and supplier of a wide range of industrial valves and components. With years of experience and expertise in the field, the company has established itself as a trusted provider of high-quality products, including the OEM Rubber Lined Gate Valve.The OEM Rubber Lined Gate Valve offered by {company name} is designed and manufactured to meet the highest industry standards. It is built with precision and incorporates innovative features and materials to ensure superior performance and longevity. The valve is engineered to handle a variety of fluids, including corrosive and abrasive substances, making it an ideal choice for demanding industrial applications.The rubber lining inside the valve provides a reliable seal, offering exceptional resistance to corrosion and wear. This feature is especially critical in environments where the flow of corrosive materials or abrasive particles is prevalent. The rubber lining also contributes to the valve's smooth operation, reducing friction and minimizing the risk of damage to the internal components.One of the key advantages of the OEM Rubber Lined Gate Valve is its versatility. It can be used in a wide range of applications, including controlling the flow of water, slurry, chemicals, and other fluids. The valve is designed to provide precise flow regulation, ensuring optimal performance and efficiency in industrial processes.In addition to its exceptional durability and performance, the OEM Rubber Lined Gate Valve is also designed with ease of maintenance in mind. This makes it a cost-effective solution for industrial facilities, as it minimizes downtime and reduces the need for frequent repairs and replacements.{Company name} takes great pride in its commitment to delivering reliable and high-quality products to its customers. The OEM Rubber Lined Gate Valve is a testament to this dedication, as it embodies the company's ethos of excellence and innovation. By continuously investing in research and development, {company name} ensures that its products are at the forefront of technological advancement, meeting the evolving needs of the industry.Furthermore, {company name} places a strong emphasis on customer satisfaction, striving to provide unparalleled support and service to its clients. The availability of the OEM Rubber Lined Gate Valve is backed by a knowledgeable and responsive team that is ready to assist customers in selecting the right valve for their specific requirements.As industries continue to evolve and demand higher standards for performance and reliability, the need for superior industrial components such as the OEM Rubber Lined Gate Valve becomes increasingly critical. With its robust construction, advanced features, and exceptional durability, this valve is poised to meet and exceed the expectations of industrial professionals across various sectors.In conclusion, the OEM Rubber Lined Gate Valve offered by {company name} represents a top-tier solution for industrial applications. Its quality construction, innovative design, and versatility make it an indispensable component for industries that rely on precise flow control and uncompromising reliability. With a commitment to excellence and customer satisfaction, {company name} continues to be a trusted source for high-quality industrial valves and components.